
Kitchen Cabinets With Built In Step Stool For Sale
Kitchen Cabinets With Built In Step Stool For Sale
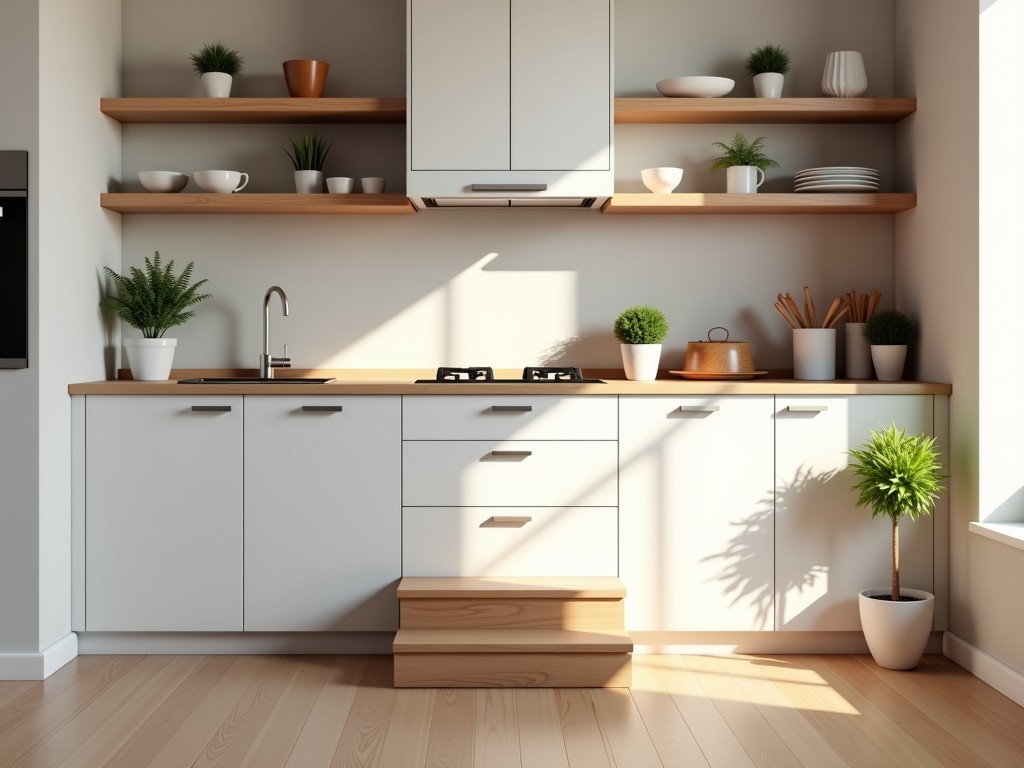
Kitchen Cabinets with Integrated Step Stool
In commercial kitchens, laboratories, and food preparation facilities, accessing upper storage safely and efficiently remains a persistent operational challenge. Standard step stools introduce tripping hazards, consume floor space, and require separate storage, disrupting workflow during peak service hours. Integrated step stool cabinets address this by combining secure, load-rated access with primary storage in a single, fixed unit—eliminating setup time and reducing injury risk associated with portable alternatives.
Engineering Perspective: Load Path and Stability
The structural integrity of an integrated step stool depends on how forces are transferred during use. Unlike freestanding stools that rely on friction and broad bases, these cabinets anchor the stepping mechanism directly to the cabinet frame, converting user load into compressive and shear forces distributed across the carcass, back panel, and wall mounting system. This design minimizes pivot points and lateral sway, critical when users reach laterally while elevated—common when retrieving items from deep shelves.
To prevent tipping, the cabinet’s center of gravity must remain behind the toe line during maximum load. Engineers achieve this by recessing the stepping surface within the cabinet’s depth, often incorporating a counterweighted rear panel or reinforcing the base with additional stiffeners. The stepping surface itself must resist deformation under repeated cyclic loading—typically 150 kg dynamic load per international safety standards for kitchen equipment—without permanent set in the substrate or finish.
Material Selection for Hygiene and Durability
Material choice directly impacts cleanliness, longevity, and compliance with food safety regulations. In environments exposed to moisture, cleaning agents, and temperature fluctuations, substrates must resist swelling, delamination, and microbial growth. Marine-grade plywood with phenolic resin overlay or high-density polyethylene (HDPE) cores are common in wet zones, while particleboard with melamine facing suffices in dry, low-humidity prep areas—provided edges are sealed with PVC or ABS banding to prevent moisture ingress.
The stepping surface requires a non-slip, wear-resistant finish. Options include textured laminate with aluminum oxide grit, rubberized coatings, or stainless steel inserts with diamond-pattern embossing. These surfaces maintain coefficient of friction above 0.6 even when wet, reducing slip risk. All exposed edges and joints must be seamless or fully sealed to prevent harborage points for pests or contaminants, aligning with HACCP and NSF/ANSI 2 standards.
Manufacturing Process and Tolerance Control
Precision in manufacturing ensures the stepping mechanism operates smoothly and safely over the product lifecycle. Cabinet panels are cut to ±0.5 mm tolerance using CNC routers to maintain square alignment—critical for drawer glides and door hinges that share the same carcass. The stepping mechanism, whether a fold-down tread or pull-out tray, relies on guided motion via steel rollers or nylon bushings mounted in precision-bored holes; deviations beyond ±0.3 mm can cause binding or uneven wear.
Reinforcement points—such as where the step attaches to the side panels—are often fortified with metal brackets or laminated hardwood inserts, installed during assembly using torque-controlled fasteners to avoid over-compression of the substrate. Edge banding is applied via hot-air extrusion to ensure uniform adhesion, preventing peeling under thermal cycling. Each unit undergoes functional testing: 500 cycles of step deployment and retraction under load, followed by visual inspection for misalignment or surface damage.
Typical Specifications
| Parameter | Typical Value |
|---|---|
| Overall Height | 800–2200 mm (customizable) |
| Stepping Surface Dimensions | 300–400 mm (W) × 250–350 mm (D) |
| Load Capacity (Dynamic) | 150 kg (tested to EN 14183) |
| Step Mechanism Type | Pull-out tray, fold-down tread, or sliding platform |
| Substrate Materials | Marine plywood, HDPE core, melamine-faced particleboard |
| Surface Finish | Textured laminate, rubber coating, stainless steel inset |
| Edge Protection | PVC, ABS, or 3mm solid wood banding |
| Mounting Options | Wall-mounted, base cabinet, or island-integrated |
Application Scenarios: Where Integrated Access Adds Value
In high-volume restaurant kitchens, these cabinets are frequently installed beside cooking lines or pastry stations, allowing staff to access ingredient bins or equipment stored above counter height without leaving their work zone. This reduces transit time and minimizes cross-traffic in congested areas. In pharmaceutical or laboratory settings, the sealed, wipe-down surfaces and absence of crevices support contamination control protocols, while the fixed installation eliminates the need to store and retrieve portable stools that could compromise clean zones.
Facility managers report reduced incident rates related to falls from portable stools after integration, particularly in environments where staff work extended shifts and fatigue increases risk of misstep. The fixed nature also ensures the stepping aid is always available—no misplaced or borrowed units—supporting consistent adherence to safety protocols.
Customization Options for OEM and Project Buyers
Customization begins with the cabinet’s role in the overall layout. Dimensions are tailored to match adjacent units, ensuring seamless alignment of countertops, doors, and drawers. The stepping mechanism can be configured for left- or right-hand operation, with varying travel distances to accommodate different user heights or storage depths. For OEMs supplying modular kitchen systems, standardized mounting interfaces allow integration into product lines without redesigning adjacent components.
Surface finishes are selected based on cleaning regimens—antimicrobial laminates for healthcare, chemical-resistant coatings for industrial kitchens, or brushed stainless for premium architectural projects. Hardware choices, including soft-close dampers on the step mechanism and load-rated hinges, are specified per cycle life expectations. All customizations are supported by engineering review to validate load paths, deflection limits, and finish compatibility with intended use.
Packaging, Logistics, and Installation
Units are shipped fully assembled or in knock-down (KD) format depending on destination and handling constraints. KD versions use cam-lock and confirmat fasteners for repeatable assembly, with alignment pins to ensure squareness. Each cabinet is wrapped in polyethylene foam and corner-protected, then placed in double-wall corrugated cartons with edge reinforcement. Palletized shipments include stretch wrapping and top/bottom protector boards to prevent damage during transit.
Installation requires anchoring to wall studs or structural backing using manufacturer-specified brackets—critical for load-bearing integrity when the step is in use. Clearance checks are performed to ensure the deployed step does not interfere with doors, drawers, or adjacent appliances. Leveling is verified within ±2 mm across the base to prevent twisting of the carcass under load. Adjustable feet or shims are provided for uneven floors.
Quality Control and Testing Protocol
Quality assurance focuses on functional safety and surface integrity. Every batch undergoes raw material verification: moisture content in wood substrates (target 8–12%), density checks for HDPE cores, and adhesion testing of laminates via cross-hatch and tape methods. Dimensional audits are conducted on the first piece of each production run to confirm CNC program accuracy.
Functional testing includes:
- Static load test: 200 kg applied to stepping surface for 10 minutes with zero permanent deflection
- Dynamic cycle test: 1,000 extend/retract cycles at 50 kg load
- Lateral force test: 150 kg applied at 45° angle to simulate reach-and-lift motion
- Surface wear test: abrasion resistance measured via Taber equivalent, targeting <50 mg loss after 500 cycles
Final inspection includes joint integrity, edge band adhesion, and smooth operation of all moving parts. Units failing any test are segregated for root cause analysis before reprocessing or scrapping.
Selection Guide for Procurement and Engineering Teams
Begin by defining the operational environment: exposure to water, cleaning agents, temperature extremes, and required hygiene level. This narrows substrate and finish options. Next, assess the required step dimensions and load profile—consider not just maximum weight but dynamic forces from movement. Confirm mounting compatibility with wall structure and adjacent cabinetry.
Request samples of stepping surfaces to evaluate slip resistance under wet conditions. Review cycle test data and warranty terms related to mechanism fatigue. For OEM inquiries, provide CAD models or layout sketches to validate integration feasibility. Always confirm that the supplier’s quality control includes the functional tests outlined above—reliability hinges on validated performance, not just appearance.
Call to Action
Share your project specifications, including layout drawings, environmental conditions, and load requirements, for a detailed engineering review and customized proposal. Our team will assess material options, mechanism types, and mounting solutions to ensure seamless integration and long-term performance in your facility.


