
Built In Kitchen Pantry Cabinet Factory Sale
Built In Kitchen Pantry Cabinet Factory Sale
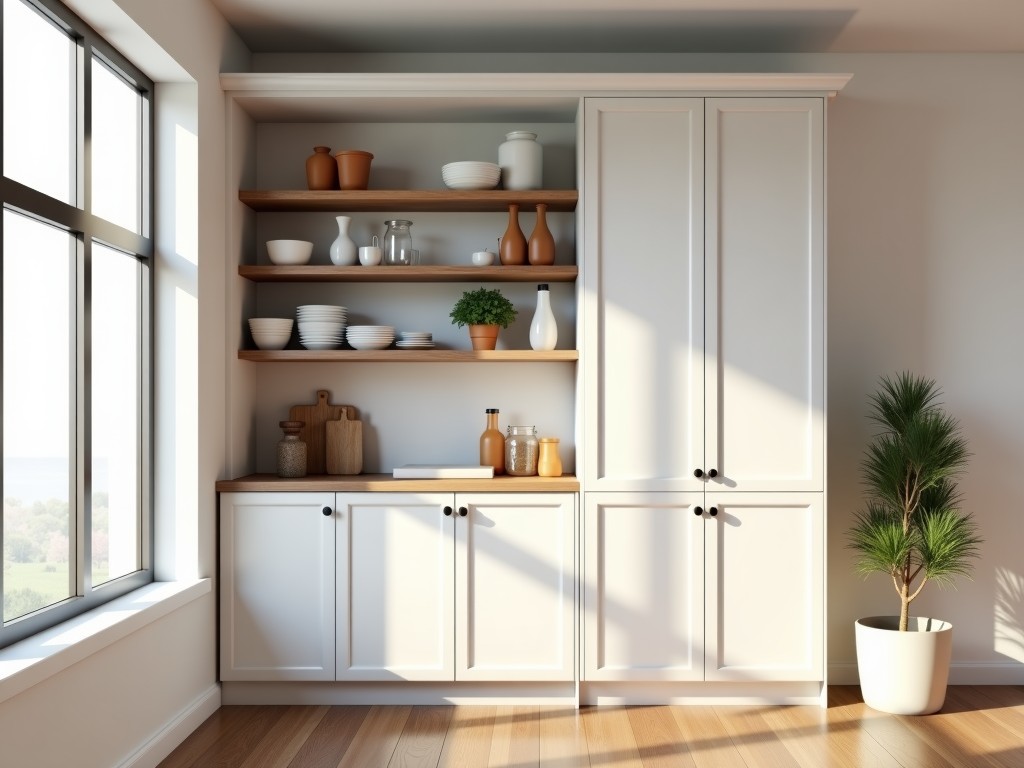
Industrial-Grade Built-In Kitchen Pantry Cabinetry Systems
In high-volume commercial and residential environments, the built-in pantry cabinet serves as a critical infrastructure for spatial optimization. Unlike modular freestanding units, integrated built-in systems are engineered to withstand significant static and dynamic loads while maintaining dimensional stability over years of operational use. Engineers and procurement teams must prioritize structural integrity, moisture resistance of core materials, and the cycle life of mechanical hardware to ensure long-term ROI and minimize maintenance costs.
Material Selection and Structural Integrity
The performance of a pantry cabinet is largely dictated by the substrate material. In industrial-spec kitchen environments, standard particleboard often fails in high-humidity zones due to swelling and delamination. Professional-grade solutions utilize high-density fiberboard (HDF) or moisture-resistant plywood to prevent warping under heavy shelf loads.
- Marine-Grade Plywood: Offers superior screw retention and resistance to water ingress for heavy-duty storage applications.
- Melamine-Laminated Board (MLC): Provides a scratch-resistant, easy-to-clean surface ideal for high-frequency contact areas.
- Edge Banding Technology: Utilization of PVC or ABS heat-reactive edging to prevent moisture from penetrating the core material.
Engineering Specifications and Load Capacity
Load distribution in a pantry system is determined by shelf span and support mechanism. Standard consumer-grade adjustable pins may shear under the weight of bulk dry goods or heavy kitchen equipment. Our built-in systems utilize reinforced shelf cleats and calculated span limits to prevent deflection (sagging) over time.
| Specification | Standard Grade | Industrial/Premium |
|---|---|---|
| Carc Thickness | 15mm - 18mm | 18mm - 25mm (Reinforced) |
| Hardware Rating | Standard Zinc-plated | Soft-close / 100k+ Cycle |
| Shelf Load Capacity (Avg) | Up to 15kg | Up to 50kg (Fixed Support) |
| Back Panel Thickness | 3mm | 6mm - 9mm (Rabbed) |
Mechanical Performance and Hardware Integration
The interface of the built-in pantry depends on the hinge and drawer slide technology. For frequent-use applications, we specify multi-directional hinges with 3D adjustment to ensure perfect door alignment even after the building settles. This prevents mechanical stress caused by misalignment, the leading cause of premature hardware failure in cabinetry systems.
Integration into existing architectural voids requires precise tolerances. Our built-in units are designed with adjustable scribes and frames, allowing installers to account for non-plumb walls while maintaining a seamless fit that prevents dust accumulation and pest ingress.
Customization and OEM Capabilities
Procurement managers for large-scale projects often require specific configurations that deviate from standard catalogs. We provide comprehensive customization options to meet precise architectural blueprints and site-specific requirements:
- Custom Internal Configurations: Optimized for floor-to-ceiling vertical utilization.
- Integrated Lighting Channels: Recessed LED profile channels with motion sensors for high-visibility storage.
- Finish Customization: Options ranging from high-pressure laminates (HPL) to architectural-grade wood veneers.
Quality Control and Logistics Standards
To ensure delivery-ready quality, every unit undergoes a dimensional inspection to verify squareness and edge-bandinging adhesion integrity. Packaging utilizes reinforced corrugated moisture-stabilized crates for international export shipments, mitigating the risk of impact-related damage during long-haul transit.
Ready to specify your pantry system?
Whether you are managing a large-scale commercial development or require a high-specification custom kitchen solution, our engineering team can provide the technical data sheets and drawings necessary for your project.
Request Technical Specifications & Quotation

