
Blue Built In Cabinets Design Wholesale
Blue Built In Cabinets Design Wholesale
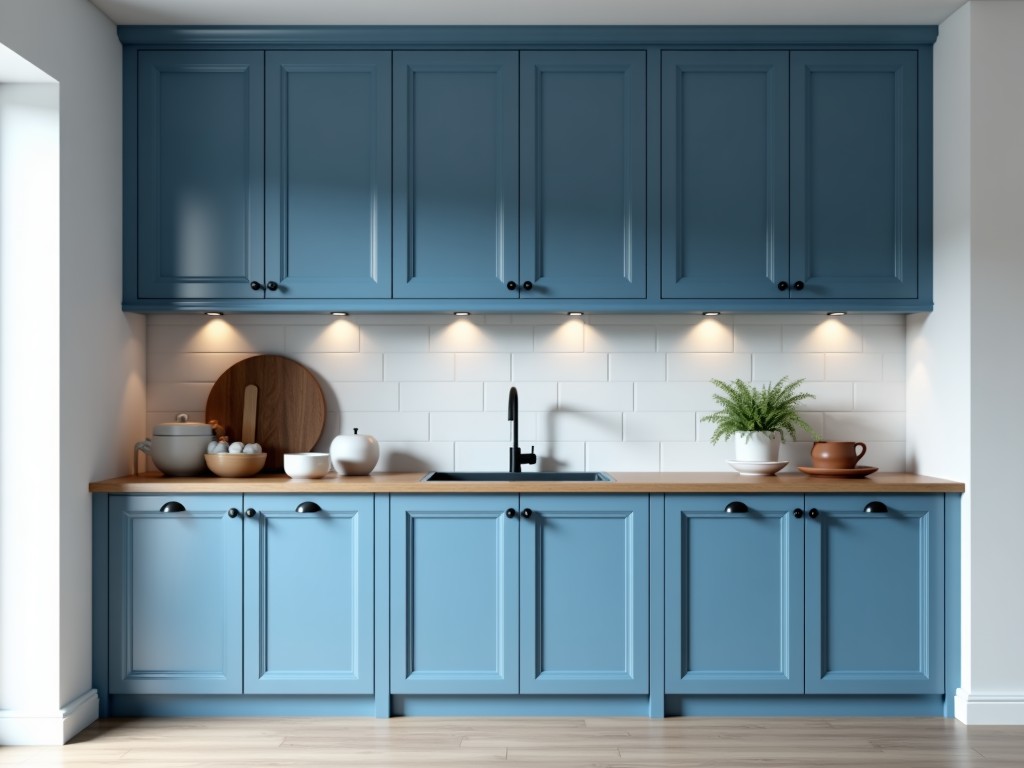
Engineering Specifications and Design for Blue Built-In Cabinetry
In industrial and commercial interior design, the selection of built-in cabinetry extends beyond mere aesthetic preference. While the blue hue is often chosen for branding or psychological impact, the engineering execution of these units focuses on material stability, load-bearing capacity, and chemical resistance within specific operational environments. High-performance blue built-in cabinets require a deep understanding of how surface finishes interact with substrates to ensure long-term dimensional consistency and color retention under high-traffic zones.
Substrate Selection and Structural Integrity
The foundation of any built-in system determines its service life. For commercial-grade cabinetry, we evaluate between high-density fiberboard (HDF) and moisture-resistant plywood based on the humidity levels of the installation. When specifying blue finishes, the porosity of the substrate is critical to prevent pigment bleeding or delamination of the decorative layer during thermal expansion or contraction cycles.
- Marine Plywood: Ideal for high-moisture environments where structural rigidity against warping is paramount.
- Melamine-Laced Particle Board: A cost-effective solution for dry office environments, provided edge-banding is ultrasonically welded.
- MDF (Medium Density Fiberboard): Utilized for complex routed profiles where a perfectly smooth surface for painting is required.
Surface Finish Engineering and Pigment Stability
Achieving a consistent blue finish that resists UV fading and mechanical abrasion requires specialized coating technologies. In industrial applications, we typically utilize high-pressure laminates (HPL) or polyurethane coatings. Unlike consumer-grade paints, these finishes offer a high impact-resistance rating, ensuring that the blue tone remains uniform despite years of exposure to cleaning agents and physical impact.
| Technical Specification | Standard Industrial Range | Primary Benefit |
|---|---|---|
| Core Panel Thickness | 18mm - 25mm | Load-bearing for heavy shelving. |
| Surface Rating | 3H to 5H Pencil Scale equivalent | Resistance to scratches and wear. |
| Hardware Grade | Soft-close / Heavy-duty | Operational longevity in high-use. |
| UV Resistance Tolerance | ASTM D458 Rating | Prevents color shifting in sunlight. |
Integration and Installation Logic
Built-in cabinetry must be integrated with the existing architectural envelope. Our design process accounts for wall plumbity, floor leveling, and MEP penetration points by utilizing adjustable fastening systems. For large-scale rollouts, we utilize a modular carcase construction which allows for rapid on-site assembly while maintaining the precision of factory-finished edges.
Procurement teams should note the importance of hardware compatibility. We specify stainless-steel hinges and drawer slides to ensure that the blue-finished cabinetry does not suffer from internal corrosion, especially in coastal or laboratory-grade environments.
Application Scenarios
Corporate Environments
Utilizing deep-toned blue cabinetry to create a focused atmosphere in conference rooms and executive suites while maintaining high durability for office storage.
Technical Laboratories
Chemical-resistant finishes designed for storage that must withstand frequent sanitation protocols without degrading the surface finish.
Discuss your project requirements.
Our engineering team provides detailed technical drawings and material data sheets for custom built-in projects.
Request a Technical Proposal

